Farm-to-yarn traceability
Vidarbha Premium cotton is sourced from the fields around our mill and processed in our own captive ginning units — short supply chains, full bale-level traceability.
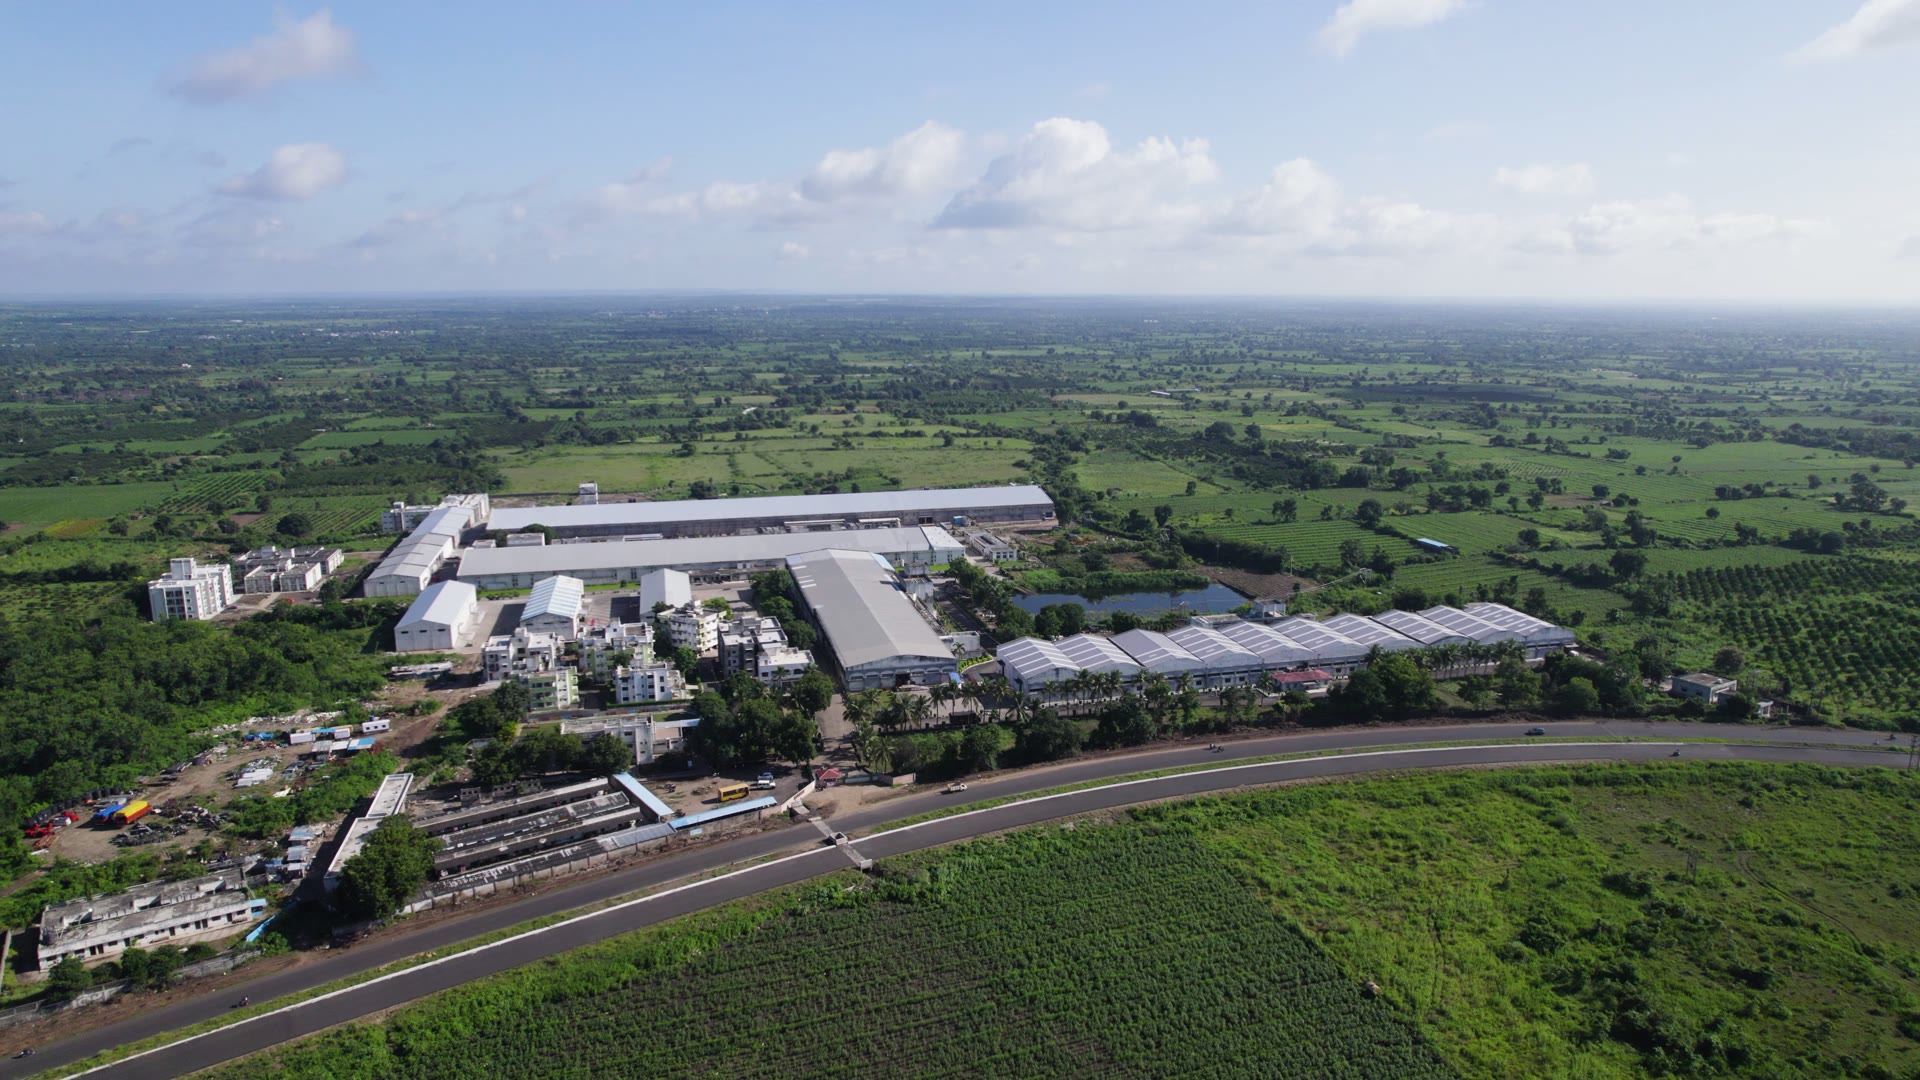
Nagpur, India · Est. 1995 · S B Rander Group
An integrated spinning mill in the heart of India’s cotton belt — turning Vidarbha cotton and cellulosic fibres into precision yarn, with a shorter, cleaner supply chain.
Sustainability
Sustainability at Sri Bhagirath isn’t a separate programme — it follows from where we are and how we spin. Local fibre, modern machinery and zero-defect quality control reduce the footprint of every kilogram we ship.
Vidarbha Premium cotton is sourced from the fields around our mill and processed in our own captive ginning units — short supply chains, full bale-level traceability.
A dedicated 14,000-spindle line spins Tencel, Modal and viscose — cellulosic fibres from managed wood sources — alone or blended with cotton.
Compact K47 ring frames, Saurer X6 autoconers and real-time spindle monitoring cut waste, rework and energy per kilogram of yarn.
Manual contamination picking, USTER Vision Shield and USTER Quantum-4 clearing mean fewer rejected fabrics downstream — the most sustainable metre is the one never re-made.
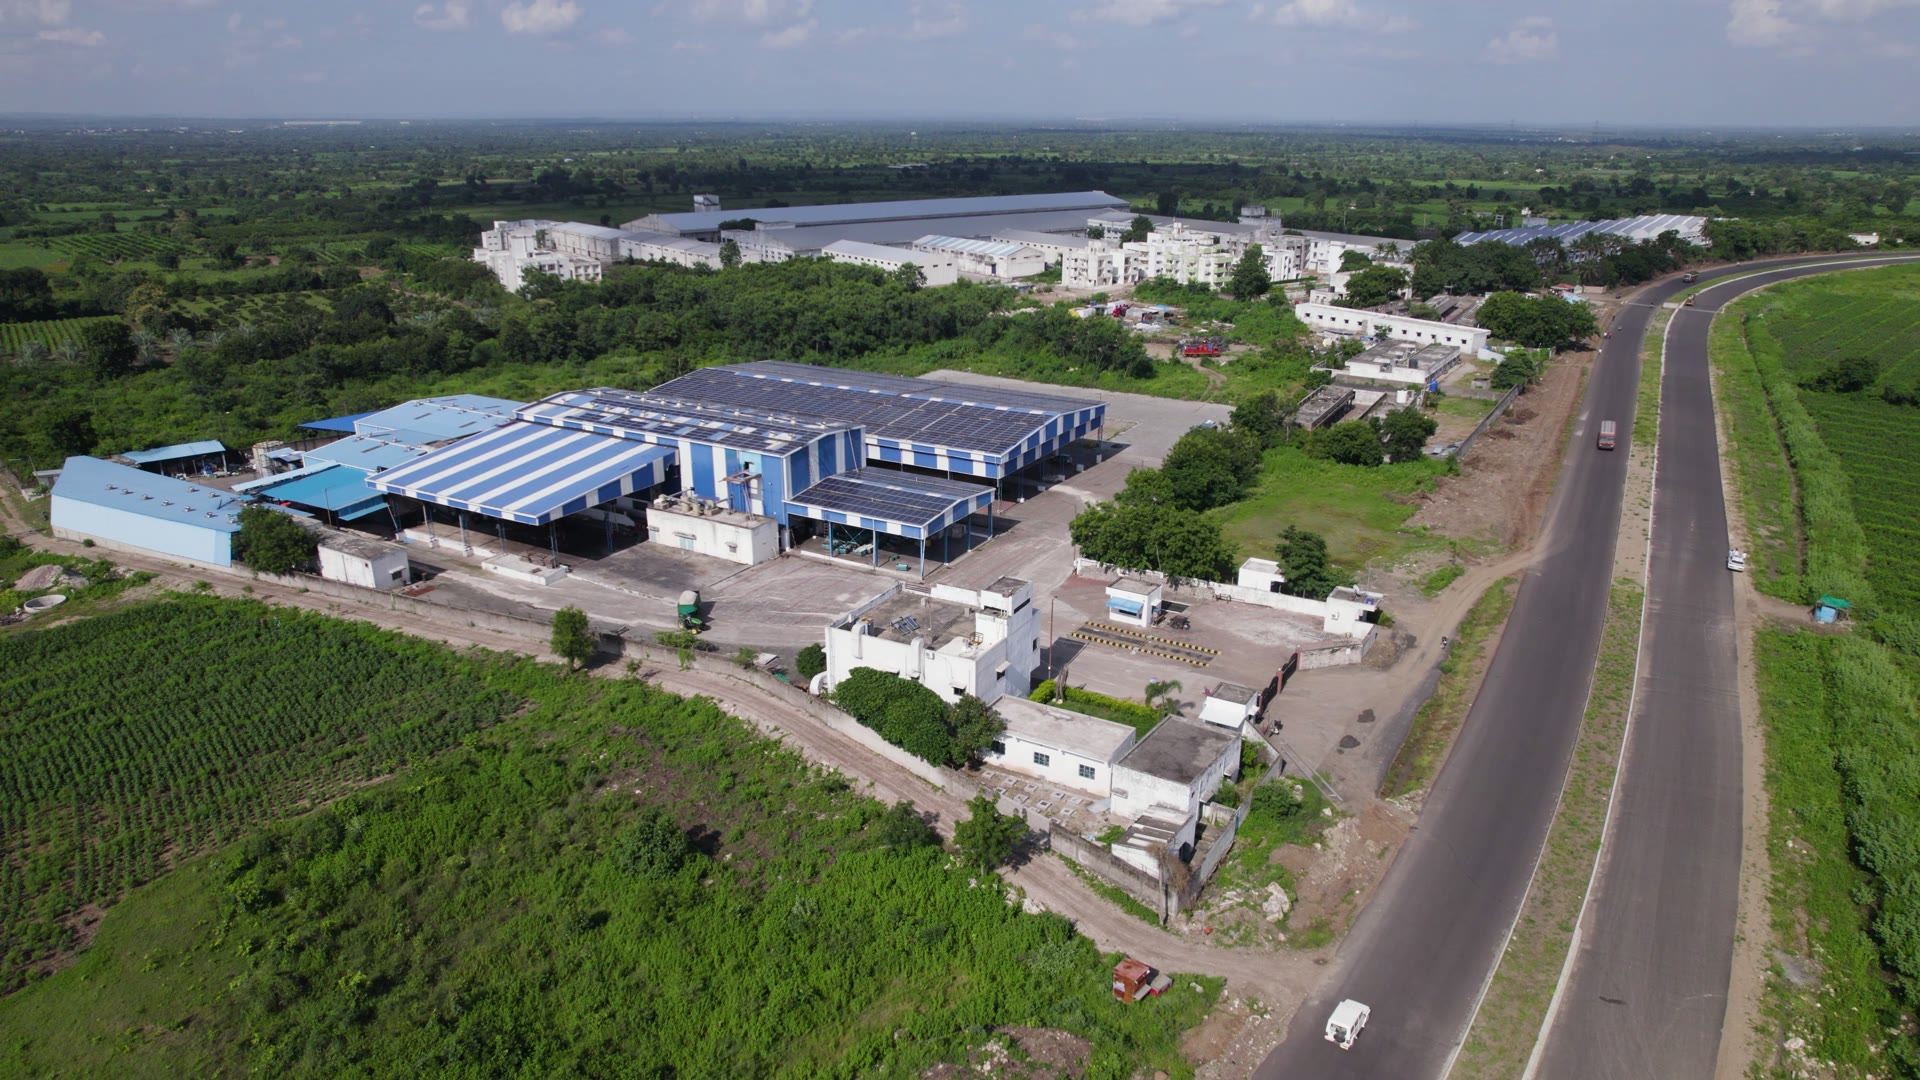
Kalmeshwar, Nagpur
Our factory sits among the cotton farms of Vidarbha. Cotton moves from field to gin to spindle within kilometres — not continents — cutting transport emissions and keeping value in the region.
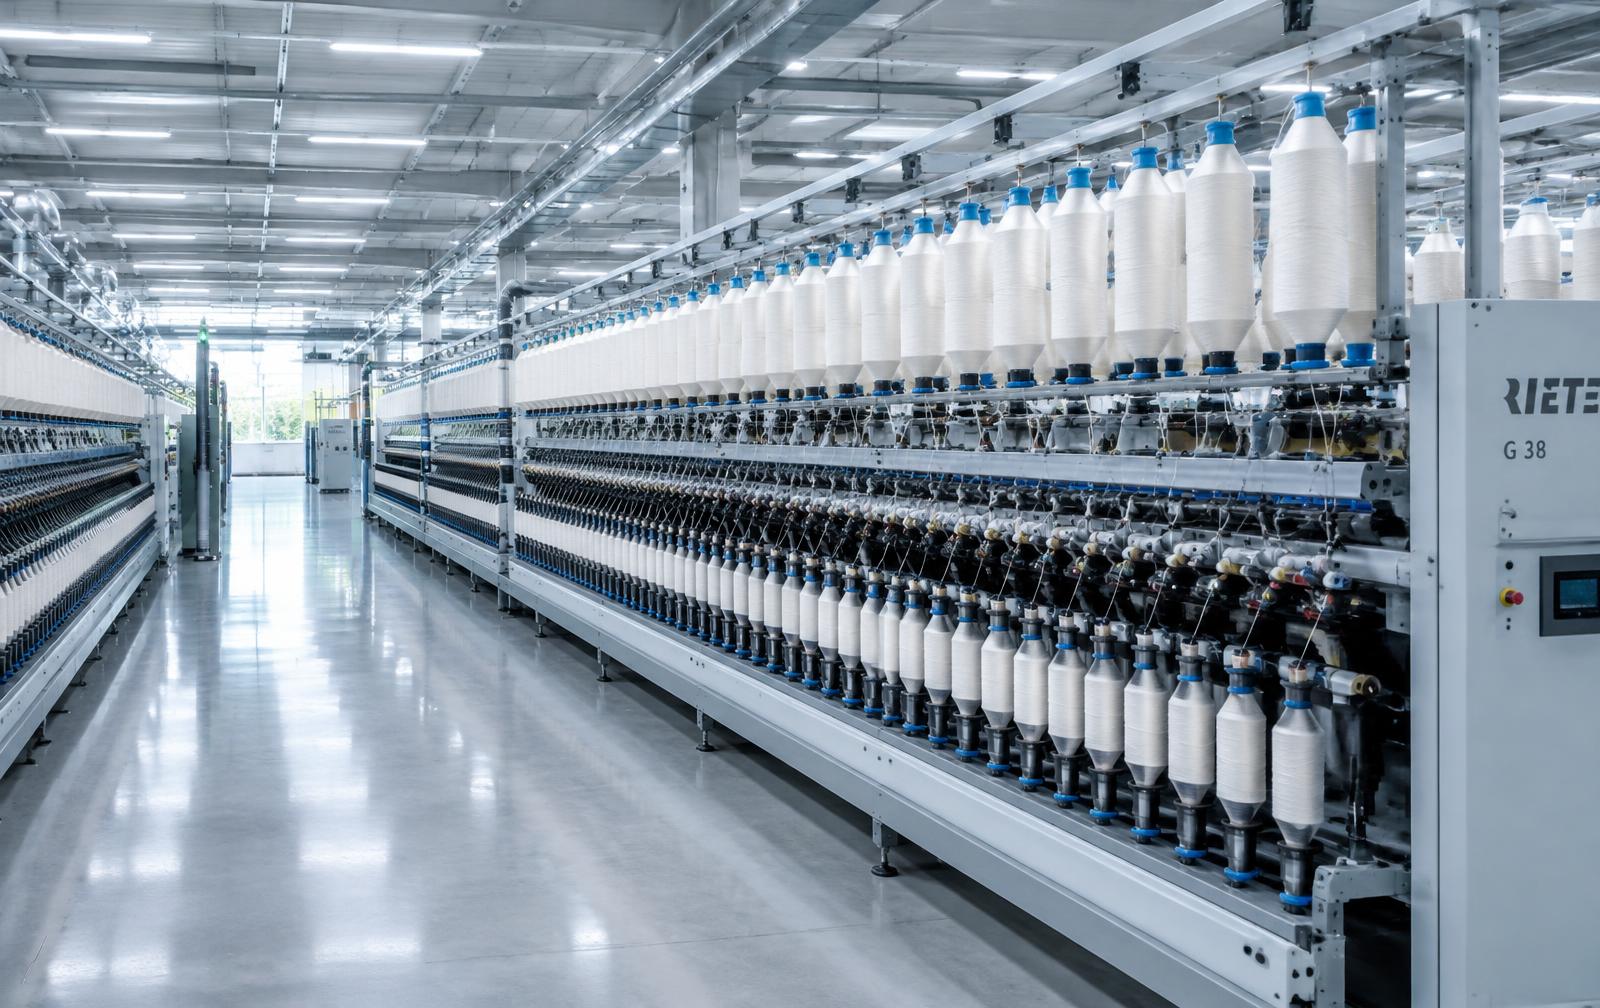
Manufacturing
Every stage — from bale to cone — runs on European precision equipment with online quality monitoring.
Products
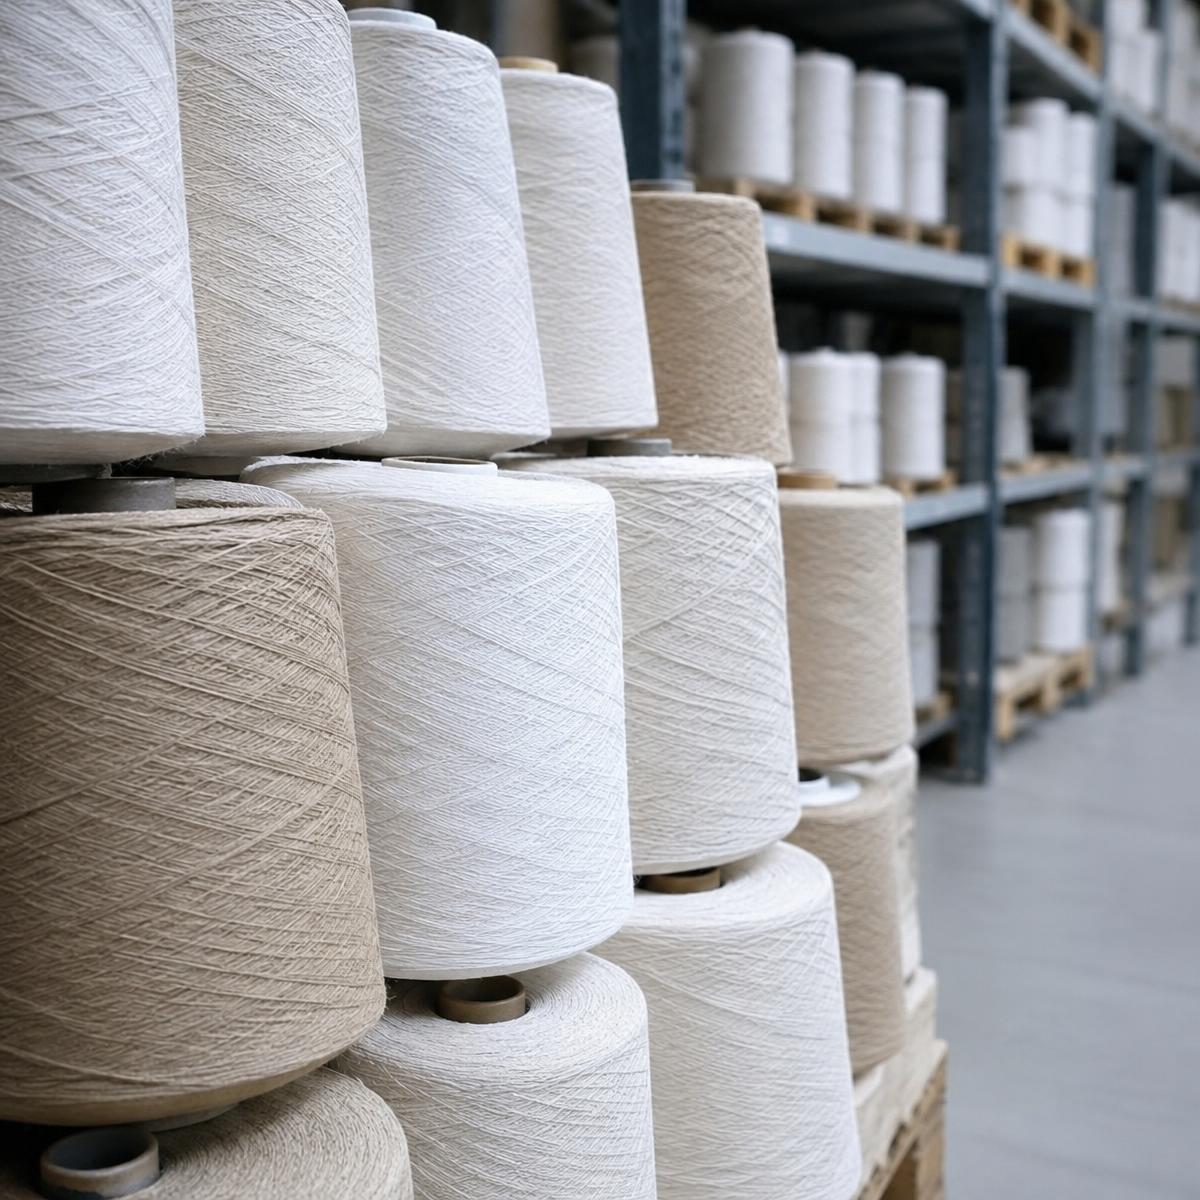
Plus an 18 MT/day knitting plant for grey knitted fabric.
About us
Established in 1995, Sri Bhagirath Textiles Ltd. is the spinning arm of the Nagpur-based S B Rander Group — a family enterprise spanning cotton trading, commodities and building materials. Three decades on, we combine deep roots in Vidarbha’s cotton economy with modern, efficient manufacturing.